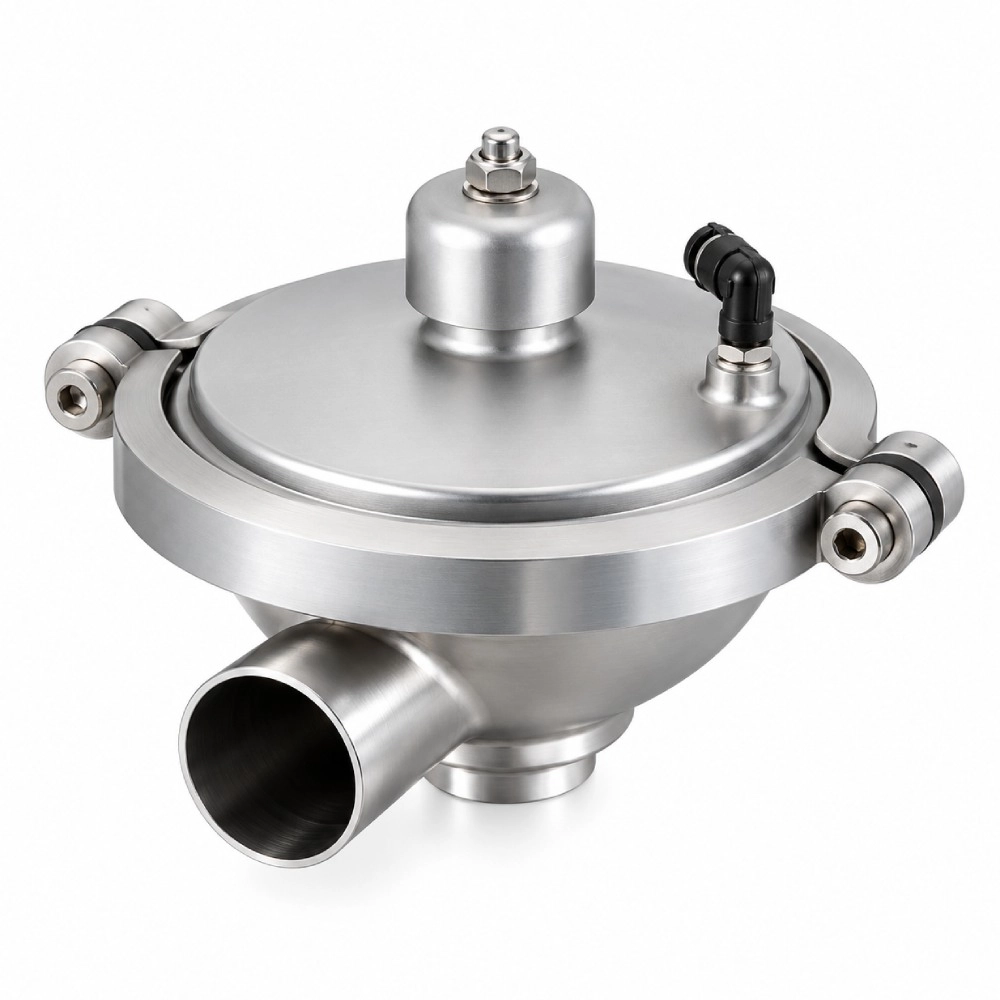
Sanitary Grade Constant Pressure Valve
Oystar Sanitary Grade Constant Pressure Valve is designed for suitable hygienic process systems requiring controlled pressure. Ideal for compatible dairy, food, beverage and pharmaceutical applications. Contact Oystar Dairy Fittings for specifications, availability and pricing.
Material Compliance & Dimensional Specifications
Standard dimensions and manufacturing tolerances adhering strictly to ASTM and sanitary standards:
The Oystar Sanitary Grade Constant Pressure Valve is designed for hygienic process systems that require controlled and consistent pressure during the transfer or processing of liquids. It can be used in suitable sanitary pipeline installations to help maintain process stability, support product quality, and improve operational efficiency.
Sanitary constant pressure valves are particularly useful in dairy, food processing, beverage manufacturing, pharmaceutical production, and other hygiene-sensitive industries. Depending on the selected model, the valve may help regulate upstream or downstream pressure in a processing line. The exact control function, operating range, connection type, and compatibility depend on the valve design.
Oystar Dairy Fittings offers sanitary process equipment for industrial buyers seeking dependable hygienic flow-control solutions. Buyers should confirm the required pressure range, product-contact materials, seal compatibility, temperature limits, connection dimensions, and cleaning requirements before placing an order.
3. Applications of Sanitary Grade Constant Pressure Valve
The Oystar Sanitary Grade Constant Pressure Valve may be suitable for the following applications, depending on the selected valve design:
- Maintaining process pressure in hygienic liquid-processing systems.
- Pressure regulation in dairy processing and milk-handling lines.
- Supporting stable pressure conditions in beverage production.
- Pressure control in food-processing pipelines.
- Maintaining suitable operating conditions in sanitary process equipment.
- Integration into compatible filling, blending, and processing systems.
- Pressure management in selected pharmaceutical and biotechnology processes.
- Use in hygienic production lines requiring cleanable, product-contact components.
Always verify whether the selected model is designed for the required pressure-control direction and process conditions.
4. Industries Where the Product Is Used
Dairy Industry: Milk processing, cream handling, yoghurt production, and dairy product manufacturing.
Food Processing Industry: Liquid food production, sauces, edible ingredients, and hygienic transfer systems.
Beverage Industry: Juice, flavoured drinks, and other beverage-processing lines.
Pharmaceutical Industry: Compatible sanitary process systems where material and regulatory requirements are met.
Biotechnology Industry: Selected hygienic liquid-processing applications.
Cosmetics Industry: Compatible liquid and cream production processes.
Industrial Process Engineering: Sanitary skids, process equipment, and pipeline assemblies.
5. Benefits of a Sanitary Grade Constant Pressure Valve
Pressure Stability: Helps maintain the required process pressure when correctly selected and installed.
Hygienic Processing: Designed for suitable sanitary applications, subject to the construction and finish of the selected model.
Improved Process Control: Supports more consistent operating conditions across compatible production lines.
Product Quality Support: Stable process conditions can help reduce unwanted variations during production.
System Integration: Can be incorporated into compatible sanitary pipelines and process equipment.
Operational Efficiency: Appropriate pressure control can support smooth process operation.
Application Flexibility: Useful across different hygienic industries when specifications are suitable.
Maintenance Planning: Selecting compatible materials and seals helps support effective inspection and maintenance.